When you think about industrial automation, you really can't ignore how important Pneumatic Valves are. These little guys are essential for controlling the flow of air and gases across a bunch of different systems. If you're buying wholesale from OEM suppliers, they can offer you custom solutions that fit your specific needs—not just a one-size-fits-all deal. Big names like Parker Hannifin and SMC Corporation are known for making top-notch pneumatic valves that you can trust. Their products help keep your operations running smoothly and reliably.
Pneumatic valves show up everywhere—think manufacturing lines, robots, even cars. They basically control how air and pressure move around, which directly impacts how well your machines work. But here’s the tricky part: choosing the right valve can feel pretty overwhelming. With so many options out there, it's easy to get stuck trying to find that perfect balance between quality and cost. That's why really understanding your needs is so important.
Looking at factors like the type of valve, what material it's made from, and what it needs to do can help you make smarter decisions. Still, keep in mind— not every pneumatic valve fits every application. You’ve got to evaluate what’s just right for your specific situation to avoid wasting money or ending up with something that doesn’t quite cut it. Chatting with experts and diving into technical specs can make a huge difference and help you pick the best solution without all the guesswork.
Definition of Wholesale OEM Pneumatic Valve Products
Wholesale OEM pneumatic valve products play a vital role in various industries. These valves control the flow of air or gas. They are essential in areas like automation, manufacturing, and chemical processing. Their design ensures efficiency and reliability under pressure. Often made from durable materials, they withstand harsh conditions.
When selecting pneumatic valves, it's crucial to assess specific needs. Different applications may require unique specifications. Consider factors such as pressure ratings and flow requirements. Quality assurance is essential in wholesale transactions. A reliable supplier can provide comprehensive testing certifications.
Tips: Prioritize valves that undergo stringent testing. These will ensure longer service life. Regular maintenance checks also prevent unexpected failures, ensuring smooth operations. Always ask for detailed technical documentation to understand each product's capabilities.
Key Components of Pneumatic Valves in Wholesale Manufacturing
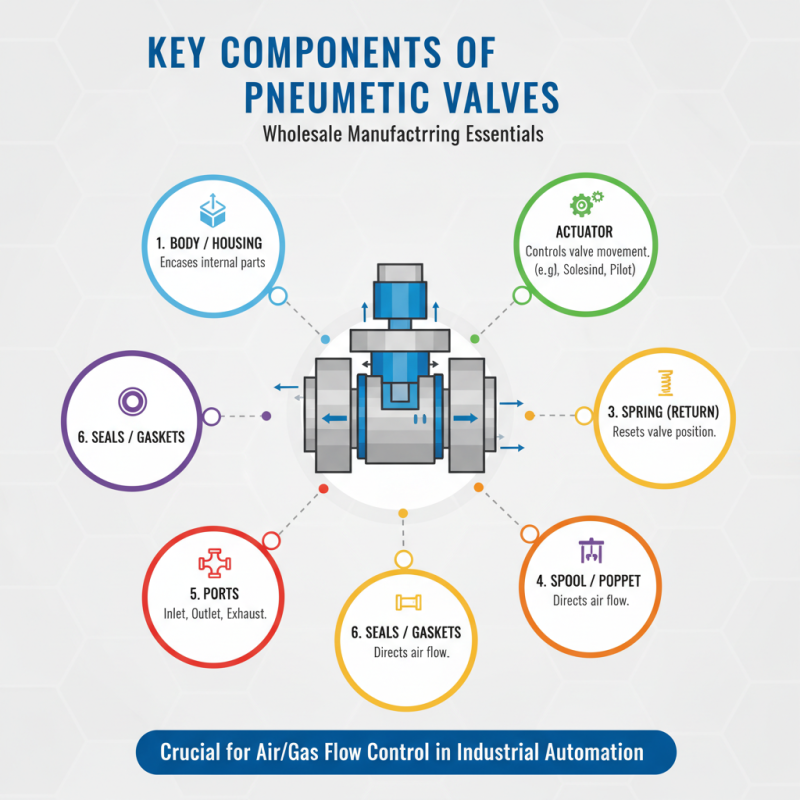
Pneumatic valves play a crucial role in various industrial applications, particularly in the manufacturing sector. These valves control the flow of air or gas in pneumatic systems. Understanding their key components is essential for effective wholesale manufacturing.
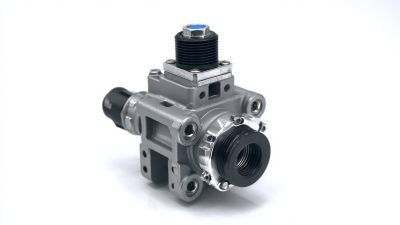
The main components of pneumatic valves include the body, actuator, seals, and spool. The body houses the valve mechanisms. An actuator operates the valve, providing precise control. Seals are crucial for preventing leaks, ensuring reliability. The spool shifts the air flow direction. This intricate design allows for efficient control of fluid dynamics in different systems.
Tips: Always ensure components are compatible before installation. Testing the valves after assembly can prevent future issues. Regular maintenance checks can prolong their lifespan.
In addition to these core components, a Pneumatic Steam Valve is vital in applications requiring steam control. Integrating this valve optimizes processes in environments like food production and chemical processing. However, it’s important to select the right specifications for each application. Open discussions with suppliers can lead to improved choices and better efficiency.
Benefits of Using OEM Pneumatic Valves in Various Industries
OEM pneumatic valves are gaining traction across various industries. These components streamline operations, ensuring efficiency and reliability. They are designed for specific applications, allowing for tailored performance. This customization leads to improved reliability and decreases downtime in manufacturing processes.
Using OEM pneumatic valves offers significant benefits. They often integrate advanced technologies, enhancing control and precision. For instance, the Pneumatic Servo Valve can provide rapid response times. This precision is critical in industries like food processing and automation. These valves not only help maintain safety standards but also optimize energy consumption.
Many companies notice the difference when switching to OEM products. However, some challenges arise with quality control and supplier reliability. It is essential to partner with reputable manufacturers. This ensures that the valves meet industry standards. Ultimately, selecting the right pneumatic solutions can drastically improve operational effectiveness.
What is Wholesale OEM Pneumatic Valve Products and Their Applications? - Benefits of Using OEM Pneumatic Valves in Various Industries
| Dimension | Description | Applications | Benefits |
| Type | Solenoid Valve | Automated machinery, Robotics | Fast response time, Low energy consumption |
| Material | Brass | Pneumatic systems, HVAC | Durability, Corrosion resistance |
| Size | 1 inch | Industrial piping, Process control | High flow capacity, Easy installation |
| Operating Pressure | 0-150 psi | Construction, Transportation | Versatility, Reliability |
| Temperature Range | -10°C to 80°C | Food industry, Chemicals | Safety, Efficiency |
Common Applications of Wholesale OEM Pneumatic Valves
Pneumatic valves are vital in numerous industries, including manufacturing and automation. These valves control the flow of compressed air, playing a key role in machinery operation. According to a report by Research and Markets, the global pneumatic valve market is expected to reach USD 2.9 billion by 2027, highlighting the growing demand.
In manufacturing, pneumatic valves manage processes such as material handling and fluid control. They are commonly used in assembly lines, ensuring efficient operation of pneumatic cylinders and actuators. The food and beverage industry also utilizes these valves to maintain product quality and safety. About 35% of pneumatic valve applications are in industries like automotive and food production, showcasing their versatility.
However, the reliance on pneumatic valves is not without challenges. Ensuring optimal performance requires regular maintenance, which can lead to downtime. Many businesses overlook the importance of routine checks. This oversight can lead to costly production halts. Continuous training for technicians is essential to mitigate issues and maximize productivity. Addressing these gaps can significantly improve operational efficiency and reduce risks in the long run.
Factors to Consider When Sourcing OEM Pneumatic Valves
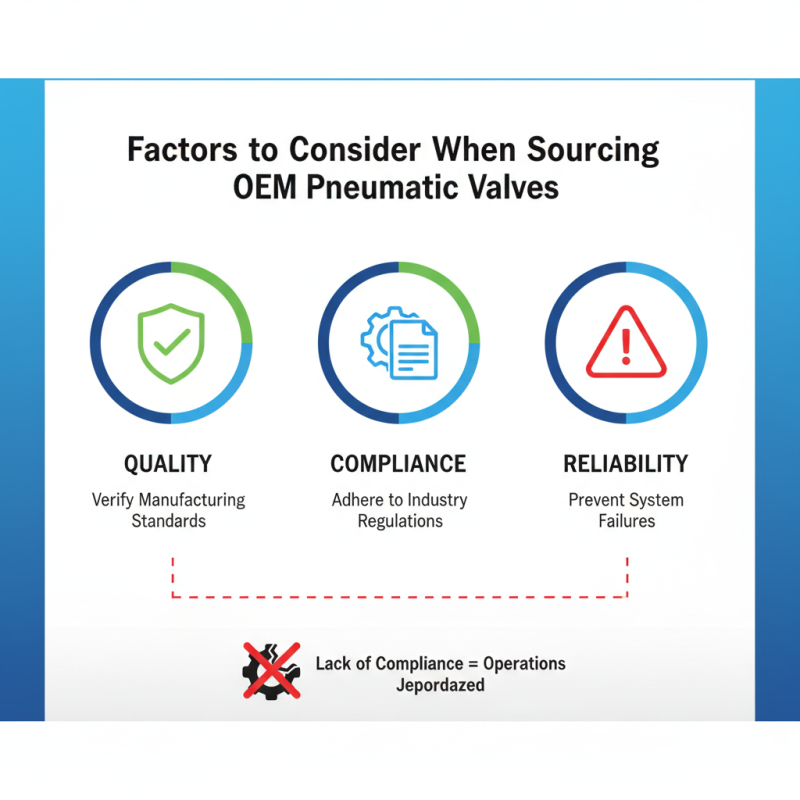
When sourcing OEM pneumatic valves, several key factors come into play. Quality is crucial. It is essential to verify the manufacturing standards. Look for valves that comply with industry regulations. A lack of compliance can lead to system failures. This could jeopardize your operations.
Cost considerations are also important. Competitive pricing often attracts attention. However, the cheapest option may not provide longevity or reliability. Evaluate the total cost of ownership. Sometimes, paying more upfront can save money in the long run. Consider the warranty and service provisions as well.
Another element to assess is the technical support provided by suppliers. Having access to knowledgeable professionals can enhance your experience. A responsive team can resolve issues quickly. Poor support can leave you in a tough situation. Be cautious about this aspect when making your decision.
Quality Standards and Certifications for Pneumatic Valves
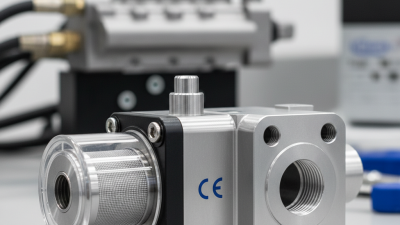
When discussing pneumatic valves, understanding quality standards and certifications is essential. These valves play a crucial role in various industries, such as manufacturing and automation. Compliance with these standards ensures safety and reliability in operation. Organizations often seek products that adhere to recognized certifications, such as ISO and CE. This not only guarantees a level of quality but also promotes confidence in their use.
For manufacturers, meeting quality standards can be challenging. Processes must be meticulously documented. Regular audits are required to maintain compliance. It's vital for companies to invest in training their staff on these standards to avoid pitfalls. Lack of knowledge can lead to errors and inefficiencies.
Tips: Always request documentation for certifications when selecting products. Look for suppliers with a robust quality management system in place. It reflects their commitment to maintaining high standards. Remember, quality products can enhance the efficiency of operations and lower maintenance costs over time. Additionally, stay updated on industry standards, as they evolve frequently.
Wholesale OEM Pneumatic Valve Products and Their Applications
This chart illustrates the different applications of Wholesale OEM Pneumatic Valve Products across various industries. The data reflects usage percentages among sectors such as Manufacturing, Automotive, Chemical, and Food & Beverage.
Future Trends in Wholesale OEM Pneumatic Valve Technology
The future of wholesale OEM pneumatic valve technology is poised for significant evolution. As industries increasingly adopt automation, the demand for efficient and reliable components, such as the Pneumatic Spool Valve, continues to surge. According to a report by Research and Markets, the global pneumatic valves market is expected to reach $8.3 billion by 2025, highlighting a robust growth trend. This increase emphasizes the critical role pneumatic components play in modern manufacturing processes.
Innovation is driving the development of smarter pneumatic systems. Industry players are investing in IoT technologies to enhance remote monitoring capabilities. Integrated sensors in Pneumatic Spool Valves can providereal-time data on performance, leading to improved predictive maintenance. Such advancements can reduce downtime drastically, as reported by a study from Deloitte, which found that predictive maintenance can decrease equipment failure by up to 30%. However, with these technologies also comes the challenge of cybersecurity risks. As systems become interconnected, vulnerabilities in data protection may arise, warranting careful consideration in future designs.
Sustainability concerns are also shaping trends in pneumatic valve technology. Manufacturers are exploring eco-friendly materials and energy-efficient designs. Some companies are even developing valves that minimize air leaks, addressing a significant efficiency loss. Nonetheless, the transition toward sustainable practices can be slow and requires substantial investment. Overall, the upcoming years will see both challenges and exciting developments in wholesale OEM pneumatic valves.
Maximizing Precision: The Role of V-420A Micro Needle Valve in Adhesive Applications
In adhesive applications, precision is paramount. The V-420A Micro Needle Valve stands out for its ability to deliver unmatched accuracy in dispensing adhesives, making it a vital tool for industries that require meticulous application. Designed with overall dimensions of 145mm x 26mm x 26mm and a weight of 277g, this valve offers a compact solution without compromising on performance. With a minimum drive air pressure of 50psi and a maximum fluid pressure of 100psi, the valve can handle a wide range of adhesive viscosities, accommodating materials from as low as 1 cps to as high as 5000 cps. This versatility is crucial in an era where the demand for customized adhesive solutions is rapidly increasing.
The V-420A achieves a maximum flow rate of 1.1 liters per minute and operates at an impressive frequency of up to 400 cycles per minute. Such specifications make it ideal for high-speed production lines, where efficiency and reliability are essential. According to industry reports, precision dispensing systems can reduce adhesive waste by up to 30%, significantly decreasing operational costs while enhancing product quality. Moreover, the valve’s fluid input, featuring a 1/8 female thread and 6-M3 screw fixing, ensures a secure and adaptable installation in various manufacturing settings, further underscoring its role in optimizing adhesive application processes.
FAQS
: They are products controlling air or gas flow in various industries, essential for automation and manufacturing.
They prevent unexpected failures, ensuring smooth operations and extending the service life of the valves.
Assess specific needs like pressure ratings and flow requirements. Always review technical documentation.
Increased automation demand, integration of IoT for remote monitoring, and innovations in sustainable designs.
IoT enhances real-time monitoring. It helps in predictive maintenance, reducing equipment failure and downtime.
Yes, interconnected systems can have vulnerabilities in data protection, requiring careful future design considerations.
Using eco-friendly materials and creating energy-efficient designs, though transitions may be slow and costly.
Valves that undergo stringent testing ensure reliability and longer service life.
It guarantees that the products meet specific standards and performance metrics for safe operation.
There is often a substantial investment required, which can slow the transition to sustainable technologies.
Conclusion
Wholesale OEM pneumatic valve products are essential components used across various industries to control the flow of gases and liquids. These valves are characterized by their robust design and efficiency, enabling manufacturers to maintain high operational standards. Key components include actuators, seals, and valve bodies, all crafted to ensure optimal performance. Utilizing OEM pneumatic valves offers significant benefits such as improved reliability, customization options, and lower production costs, making them a preferred choice in manufacturing settings.
Common applications for these valves span numerous sectors, including automotive, aerospace, and manufacturing, where precision and responsiveness are critical. When sourcing OEM pneumatic valves, factors like quality standards, certifications, and technological advancements must be considered to ensure the selection of reliable products. Overall, as industries evolve, so too does the technology behind pneumatic valves, driving innovations that cater to the increasing demands for efficiency and sustainability in operations.